OSLO Crystallizer — Fluidized Bed Cooling Crystallization System Product Overview The OSLO (Oslo) crystallizer is a continuous cooling crystallization system that utilizes a circulating mother liquor and a fluidized bed to achieve crystal growth and particle size classification. The system generates supersaturation through external circulation cooling or vacuum cooling. The supersaturated mother liquor is introduced into the fluidized bed section where it contacts existing large crystals, whic
OSLO Crystallizer — Fluidized Bed Cooling Crystallization System
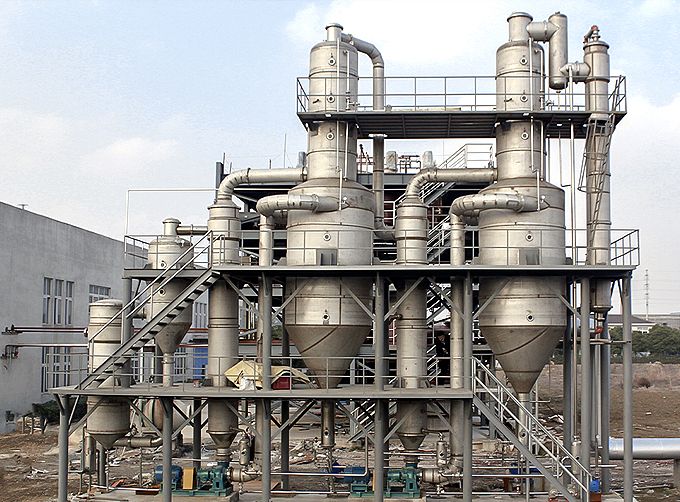
The OSLO (Oslo) crystallizer is a continuous cooling crystallization system that utilizes a circulating mother liquor and a fluidized bed to achieve crystal growth and particle size classification. The system generates supersaturation through external circulation cooling or vacuum cooling. The supersaturated mother liquor is introduced into the fluidized bed section where it contacts existing large crystals, which serve as nuclei for orderly, layer-by-layer crystal growth. A defining feature is the countercurrent contact between the crystal phase and the liquid phase under fluidization conditions: fine particles remain suspended in the upper growth zone, while large crystals settle to the bottom for discharge. This process yields crystal products with extremely narrow size distribution and exceptionally high purity. OSLO crystallizers are widely applied in fertilizer production, inorganic salts, fine chemicals, food additives, and wastewater evaporative crystallization, representing the preferred solution for high-quality crystalline products.
The feed solution is circulated by a pump into a cooler (or vacuum flash chamber), where supersaturation is generated by lowering the temperature or evaporating the solvent. The clear supersaturated mother liquor enters the bottom of the fluidized bed crystallizer and flows upward through the suspended crystal bed. During upward flow, the solute deposits evenly onto the crystal surfaces, promoting layer-by-layer growth and eliminating fine nuclei. Large crystals, whose settling velocity exceeds the upward liquid velocity, accumulate at the bottom and are discharged as product; small particles and fines remain suspended in the upper zone and continue to grow. By adjusting the circulation flow rate and cooling load, supersaturation levels and crystal growth rates are precisely controlled, enabling a tunable particle size distribution.
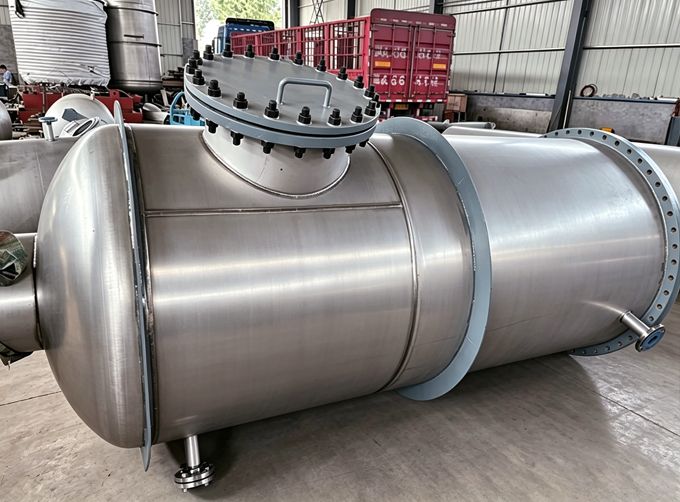
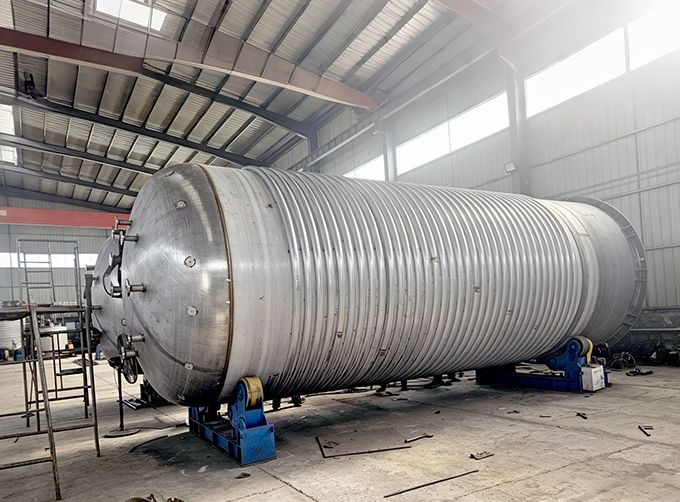
Crystallizer Body (Fluidized Bed Section) : The core of the system, providing the space for crystal suspension and hydraulic classification. The bottom section features a product discharge port, while the top section serves as a clarified overflow zone. The variable cross-section design enables size-based hydraulic classification.
Circulation Pump: Typically a high-flow, low-head axial flow pump that maintains the fluidization state and delivers mother liquor to the cooling or evaporation system.
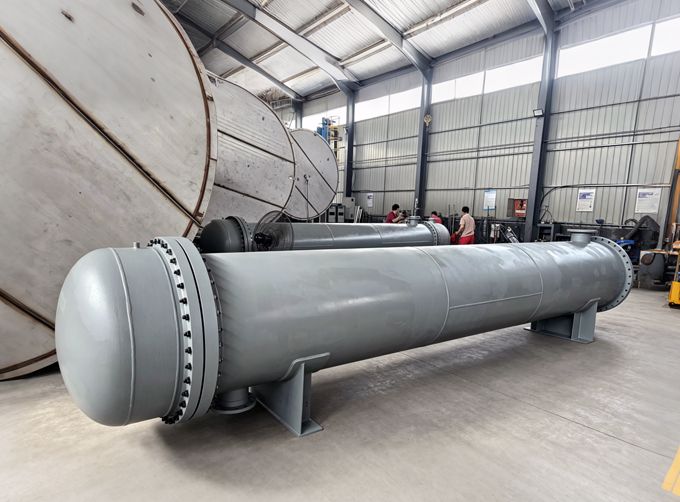
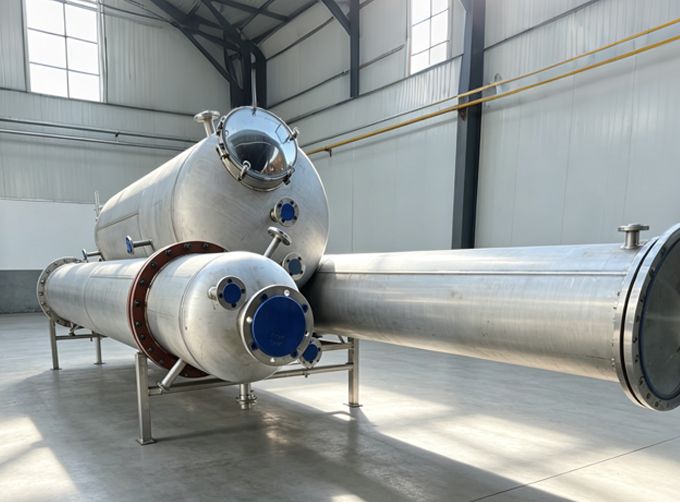
Cooler / Vacuum Flash Chamber: In external circulation cooling crystallization, a shell-and-tube heat exchanger removes sensible heat. In vacuum cooling crystallization, a flash chamber adiabatically evaporates the solvent to generate supersaturation with even lower energy consumption.
Fines Dissolver (Optional): Eliminates excess fine nuclei by mild heating or dilution, reducing secondary nucleation and further optimizing product crystal size.
Feed System & Control System: An integrated PLC/DCS platform for online monitoring of temperature, concentration, level, and flow, delivering precise supersaturation control and continuous, stable product discharge.
Uniform & Controllable Particle Size: Based on fluidized bed hydraulic classification, the system produces crystals with an extremely narrow size distribution (low C.V.). The mean particle size can be adjusted within the 0.5–3.0 mm range, yielding regular-shaped crystals with outstanding flowability.
High Purity & Low Impurity Content: The countercurrent washing effect and slow, layer-by-layer growth effectively minimize mother liquor occlusion. Product purity is significantly improved compared to conventional crystallization, and caking tendency is greatly reduced.
Continuous, Large-Capacity Operation: Single-unit processing capacities range from several to dozens of tons per hour. The process supports continuous feed and continuous product discharge, providing excellent stability for large-scale industrial production.
Low Energy Consumption: Vacuum-cooled OSLO crystallizers operate under negative pressure via adiabatic evaporation, eliminating the need for large quantities of cooling water and extensive heat exchange surfaces. The comprehensive energy consumption per ton of crystal product is significantly lower than traditional evaporative crystallization.
Flexible Operating Window: The system readily adapts to fluctuations in feed concentration and composition. Through adjustment of circulation flow, residence time, and subcooling, it flexibly accommodates changing process conditions.
High Slurry Density: The fluidized bed maintains a high crystal slurry density, providing excellent volumetric productivity with a minimized footprint and high cost-effectiveness.
Parameter Specification Range / Description |
Processing Capacity 0.5–60 t/h (product basis, customizable)
Product Crystal Size 0.5–3.0 mm (adjustable)
Crystallization 5–90 ℃ (depending on materials and coolant) Temperature
Supersaturation Control ΔC = 0.5–3.0 g/L (online adjustable) Range
Circulation Flow Ratio 0.8–3.0 times of design range (controllable)
Material of Construction SS304/316L, 2205 Duplex Stainless Steel, 904L, Titanium, etc.
Control Mode PLC/DCS automatic control, remote monitoring & data logging
Applicable Systems KCl, NH₄Cl, Na₂SO₄, (NH₄)₂SO₄, NaNO₃, KNO₃, MAP, Adipic Acid, Pentaerythritol, etc.
Fertilizer & Inorganic KCl crystallization, (NH₄)₂SO₄ granulation, Salts NaNO₃/NaNO₂ crystallization, phosphate refining
Fine Chemicals Adipic acid cooling crystallization, pentaerythritol crystallization, aromatic acid purification
Food Additives MSG crystallization, citric acid refining, sorbitol crystallization, dextrose crystallization
Pharmaceutical Active Pharmaceutical Ingredient (API) purification, amino acid crystallization, organic acid separation
Environmental & Resource ZLD evaporative crystallization for salt Recovery separation, high-salinity wastewater volume reduction
New Energy Materials Lithium salt crystallization (Li₂CO₃, LiOH), KPF₆/NaPF₆ crystallization


 1464791908@qq.com


 +86 13832176953
